
High-Temperature Aluminum Marking: Hot Surfaces, Labels and Heat Exposure
Request a solution
- Original TTR manufacturer since 2013
- Automated coating and slitting
- IQC / IPQC / OQC control
- ANSI barcode grade testing
- -20°C to 120°C environmental testing
- Batch-level traceability
- ANSI barcode grade
- Batch traceability
- RoHS / REACH compliance
- SGS and MSDS documents on request
For buyers investigating high-temperature aluminum marking, the first distinction is between applying identification to a hot surface and keeping identification readable through later heating. Direct marking and a separately printed label or tag require different compatibility checks. For an in-house thermal transfer route, qualify the receiving material, ribbon and attachment together against the actual aluminum surface and heat exposure.
Key Takeaways
- Aluminum identification can face both high surface temperatures and subsequent heat treatment.
- Thermal transfer printing uses a heated printhead to transfer ribbon ink onto a receiving material.
- A resin ribbon category does not establish compatibility with every aluminum surface.
- Temperature cycling, chemical contact and surface energy affect label adhesion.
Separate the temperature during marking from later heat exposure
High-temperature aluminum marking involves two distinct questions: whether identification can be applied at the current surface temperature and whether it remains usable after subsequent heating. The Spanish search phrase “marcaje en aluminio alta temperatura” does not specify which question the buyer needs to answer. Record both before comparing a marking process with a printable label or tag.
The distinction comes from the aluminum production environment. The supplied aluminum-marking reference identifies high surface temperatures and subsequent heat treatment as separate challenges. Another supplied reference distinguishes marking on hot surfaces from marking on cold surfaces. A process described as suitable for hot application therefore answers a different question from a printed identification system evaluated after a heat cycle.
For an initial specification, describe the sequence in ordinary production terms: when the identification is created, when it is attached or applied, when the part heats up, and when someone must read it. Ask whether reading is needed during exposure, after cooling, or at both points. These are requirements to establish for your application, rather than performance claims for a particular consumable.
Also separate the part from its identification. An aluminum component, an aluminum foil tag and a polymer label attached to aluminum describe different receiving surfaces and constructions. Do not transfer a temperature description from one of these objects to another. Start with the exact object being marked, then define the heat conditions that its identification must face.
Distinguish direct marking from a printed label or tag
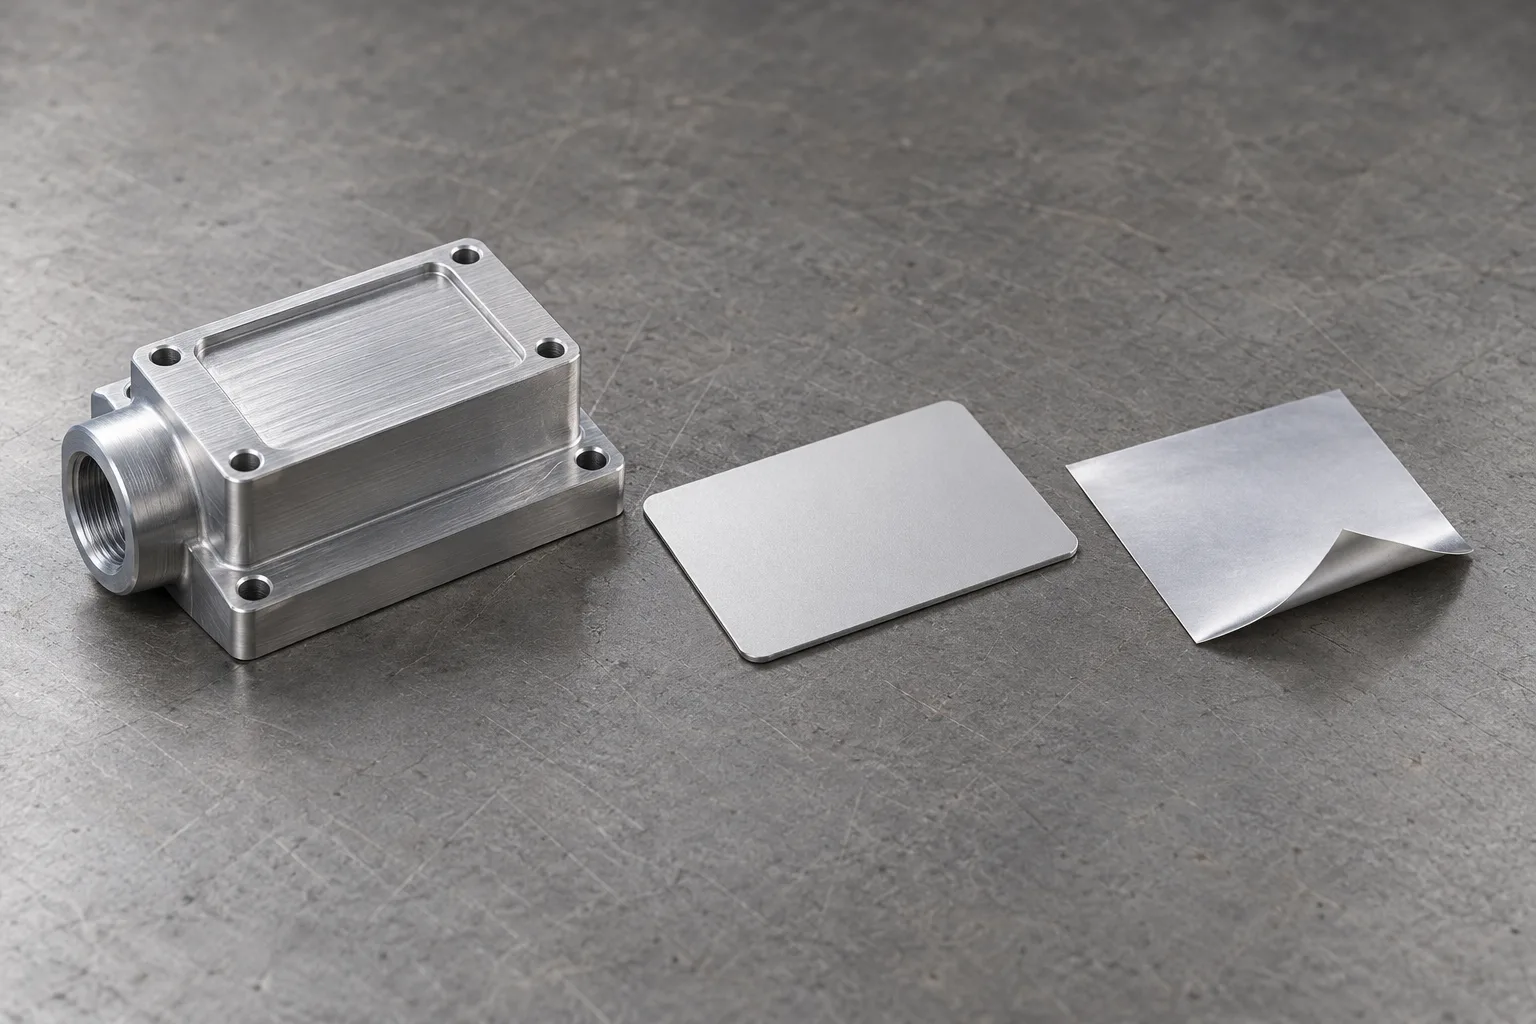
Thermal transfer printing creates an image by transferring ribbon ink under a heated printhead onto the material below it. In a label or tag workflow, that receiving material must be identified explicitly. Saying that an item is “for aluminum” leaves open whether the printer receives a printable tag or whether equipment marks the component itself.
Direct hot-surface marking is a separate route. The supplied marking-systems reference describes special paints used with a marking gun to identify a hot surface. That evidence establishes the existence of this approach; it does not establish a universal paint, operating temperature or recipe for your aluminum part. Treat a direct-marking proposal as a process requiring its own equipment and surface evidence.
For buyers who want to print identification themselves, the consumable route deserves a more precise description. The supplied special-label catalog lists aluminum plate and aluminum foil nameplate material described as directly printable by thermal transfer. It also lists aluminum foil tags with high-temperature descriptions. These entries identify product categories to investigate, rather than proving that a specific printer and ribbon can produce an approved heat-resistant barcode on them.
Use the distinction when discussing a sample with a supplier. Request the exact printable face, material format and intended attachment, then confirm which printer can handle that format. A sample of printable aluminum-based stock is a different test object from an unfinished aluminum component. If your requirement is direct identification on the component, do not approve a label sample as evidence for that requirement.
Match the ribbon to the receiving surface before approving heat resistance
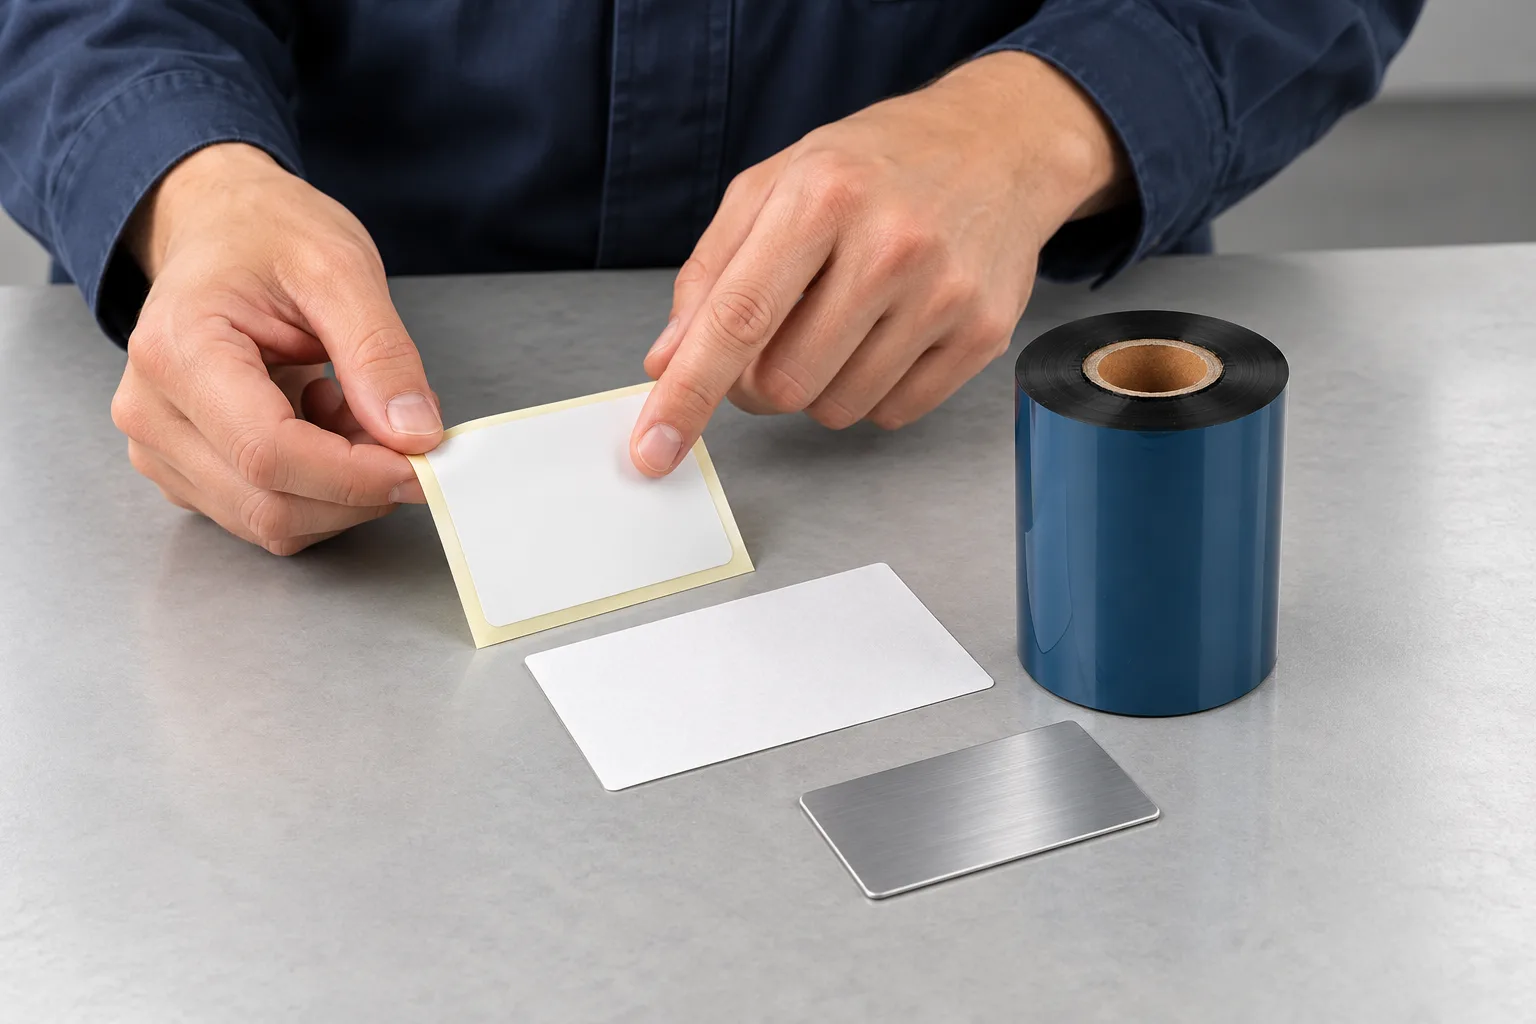
Resin formulations are designed to adhere to compatible synthetic surfaces, while wax inks generally anchor into porous paper fibers. This explains why ribbon selection starts with the receiving material rather than the word “aluminum” in an application description. Compatibility belongs to a particular ribbon and surface combination.
The supplied ribbon-selection evidence places full resin ribbons among the options for demanding synthetic films such as polyester, polyimide and vinyl. Polyimide labels are also described as having thermal stability and chemical resistance. Those descriptions make such constructions relevant to a heat-exposed label discussion, but they do not assign an operating temperature to every polyimide label or establish adhesion to your aluminum finish.
For an in-house trial, use the following sequence as a qualification brief:
- Identify the actual receiving face, including any printable coating, and name the proposed ribbon and printer.
- Write down the surface condition at attachment or marking and the later temperature profile, including duration and repeated cycles.
- Print the information that production will use, then apply or attach the sample to the same aluminum surface intended for production.
- Expose the sample to the intended process and check the required reading and attachment outcomes at the specified stages.
- Record which combination passed the agreed requirements before accepting a replacement consumable.
Keep print formation and later durability as separate checks. The supplied printing reference identifies printhead pressure, temperature, ribbon-to-substrate compatibility and speed as interacting factors in clear printing. A readable image at the printer is the starting condition for the exposure trial. It does not establish the image or attachment performance after the trial.
Data and Evidence
The available evidence supports distinctions between marking conditions, printable constructions and ribbon compatibility, but it does not provide a complete temperature-qualified aluminum printing system. The table separates what each relevant source establishes from what your sample approval still needs to establish.
| Evidence | What it establishes | What to verify for your application |
|---|---|---|
| Supplied aluminum-marking references | High surface temperatures and later heat treatment present separate marking challenges; marking may occur on hot or cold surfaces. | The application temperature and subsequent exposure sequence. |
| Special-label product catalog | Entries include thermal-transfer-printable aluminum plate or foil nameplate material and aluminum foil tags described as heat resistant. | The exact stock, receiving face, printer, ribbon and attachment. |
| Ribbon-to-substrate guidance | Wax and resin formulations have different receiving-material applications. | Image formation on the proposed printable face. |
| Adhesion guidance | Temperature cycling, chemical contact and surface energy affect adhesion. | The same material stack applied to the same aluminum surface. |
Source descriptions used here are the supplied aluminum-marking references, the Special Label Product List 20260811, and the supplied ribbon and adhesion guidance. The catalog includes aluminum foil tag entries using “350 Degrees” in their descriptions. Those entries do not supply the exposure duration or identify a tested ribbon-and-image combination, so this article does not treat that number as an approval limit.
If a trial fails, record whether the unmet requirement concerns image readability, attachment or the fit of the material in the printer. Review evidence for that part of the construction before changing the whole system. Your next step is to prepare one sample brief naming the receiving surface, printing combination, heat sequence and required reading outcome.
Frequently Asked Questions
Does high-temperature aluminum marking mean marking the metal while it is hot?
It can, but it can also refer to identification that must survive later heat treatment. Specify the surface temperature during marking separately from the subsequent exposure profile.
Can a 350-degree aluminum foil tag rating approve my printed barcode?
No. A catalog temperature description does not establish the performance of your ribbon, printed image, attachment and exposure duration together. Request conditions for the exact construction and test your printed sample.
Can I use a resin ribbon to print directly onto any aluminum part?
The resin category alone does not establish that compatibility. Confirm that the actual receiving surface and physical format are suitable for the ribbon and printer before running samples.
Recommended products for this industry

Aluminum Foil High-Temperature Label
Coated aluminum label for metal processing, heat treatment and high-temperature part…
View details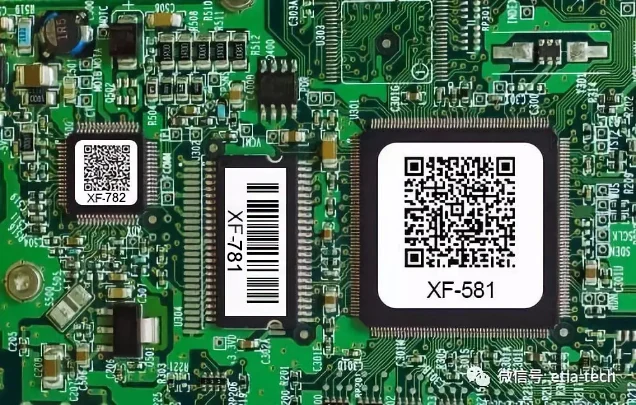
Anti-Static High-Temperature Polyimide Label
Anti-static polyimide label for ESD-sensitive electronics assembly and high-temperature…
View details
Black High-Temperature Polyimide Label
Matte-black polyimide label for high-contrast codes on dark electronics and industrial…
View details
CL-582 High-Temperature Polyimide Labels for Printed Circuit Board Traceability
CL-582 is a high-temperature polyimide (PI) label material for printed circuit board (PCB) and sensitive electronic component process control and product traceability. It has a gloss white coating, a listed thickness of 2mil and an acrylic adhesive. The source identifies wave soldering and reflow soldering as applications. Selection requires confirmation of the actual heat exposure and chemical conditions: the listed temperature range has no specified exposure duration, and solvent resistance is qualitative.
View detailsNeed the right ribbon for your label application?
Share the label material, printer and operating environment. Our team will recommend a tested combination.
